TOOL PAL: the tooling behind the part.

Seven tooling families for sheet metal production, plus the engineering and manufacturing services that support them. Built for the press, the material and the feature — not for a catalogue photo.

7 tooling families 1000 kN/m press brake rating 1.5 lakh hits on a TPP tool

The tooling brand

Not just a tool maker — your tooling buddy.

Under TOOL PAL we provide high-performance sheet metal fabrication tooling designed to improve productivity, precision and operational efficiency. Our products are developed for modern manufacturing requirements and are compatible with leading sheet metal processing equipment.

TOOL PAL

Seven families. One specification standard.

Filter by tooling family. Every enquiry is reviewed against the press, the material and the production volume before a tool is proposed.

7 results
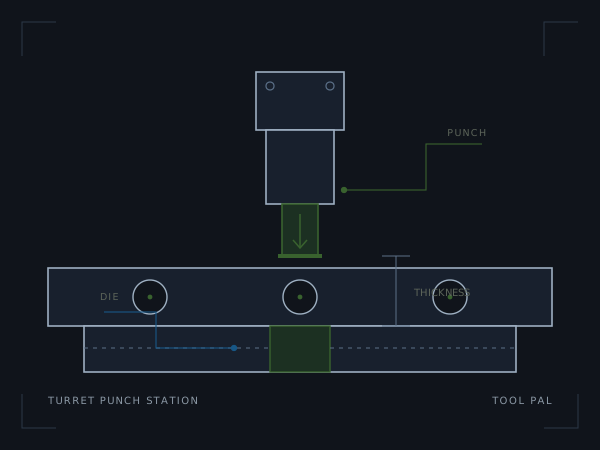
Turret punch tooling station illustration

Turret punch

Turret punch press tools

Punches, dies and strippers for turret punch presses, including special shapes, regrind support and production tooling developed around the part.

Type
Thick / thin turret
Tooling
Punch · die · stripper
Proven
1.5 lakh hits
Request this tool
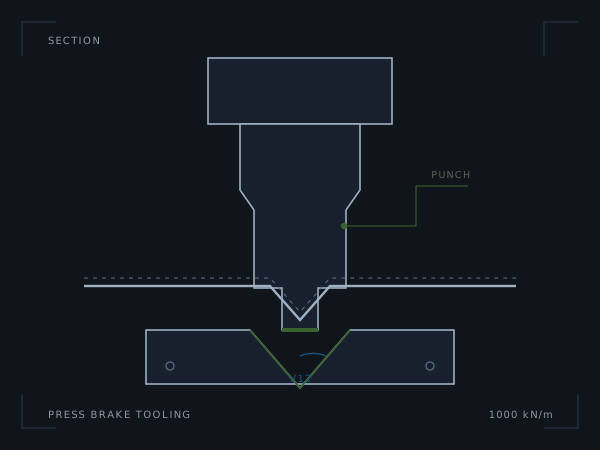
Press brake punch and V die illustration

Press brake

Press brake tools

Punches and V dies for production bending, built for repeatable angles and the loads that come with heavy sheet.

Max load
1000 kN/m
Capacity
100 t/m
Die
V12
Origin
Made in India
Request this tool
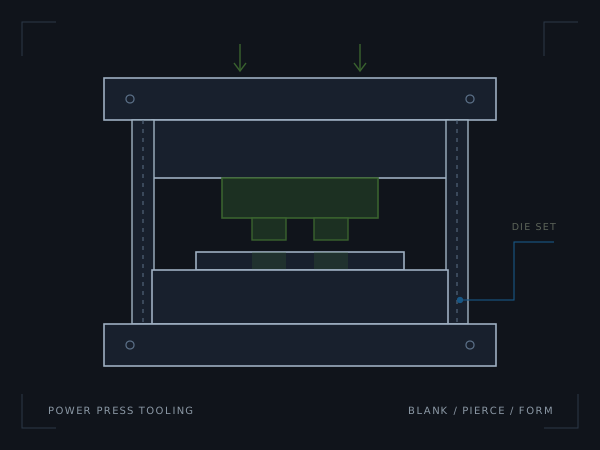
Power press die set illustration

Power press

Power press tools

Blank, pierce, form and draw tooling for conventional and hydraulic presses, matched to the press and the part.

Operations
Blank · pierce · form
Press
Conventional / hydraulic
Build
Custom die set
Request this tool
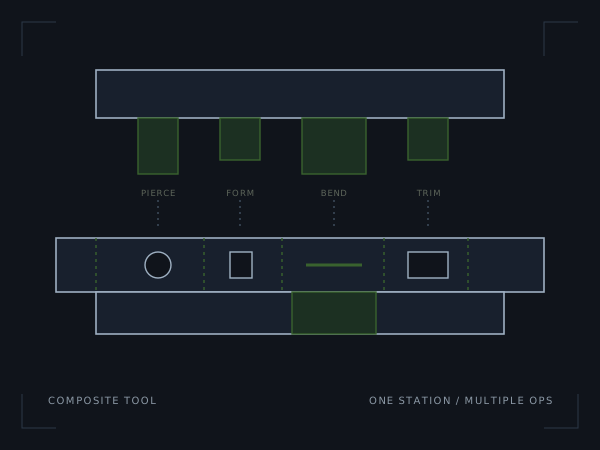
Composite tool with several operations in one station

Composite

Composite tools

Several operations completed in a single station, where cycle time and press capacity make one hit the better route.

Stations
Single
Operations
Pierce + form + bend
Best for
High volume
Request this tool
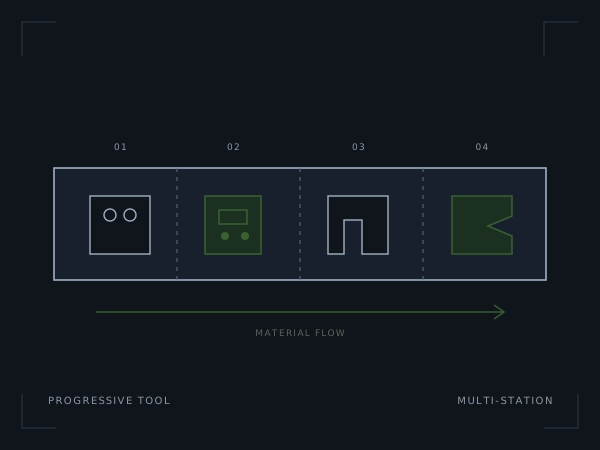
Progressive tool strip with four stations

Progressive

Progressive tools

Multi-station progression for parts where output and consistency justify the tooling investment. Strip layout is developed with the part.

Stations
Multi
Output
High volume
Material
Sheet steel / aluminium
Request this tool
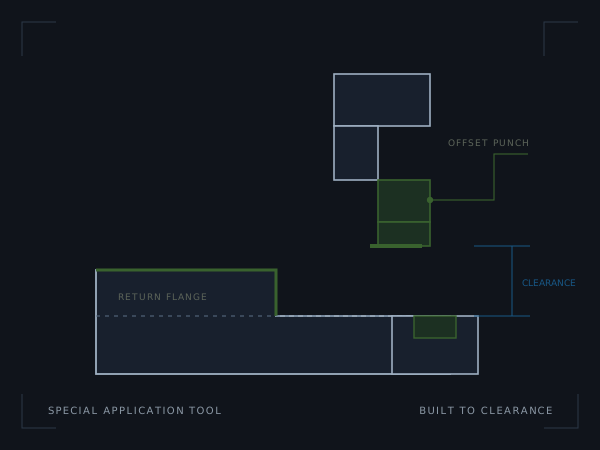
Special application offset punch and return flange

Special application

Special application tools

Tools built around an obstruction, an unusual form or a feature standard tooling cannot reach. Designed to the part and proven on a trial.

Build
To drawing / sample
Use
Obstructed features
Support
Design + trial
Request this tool
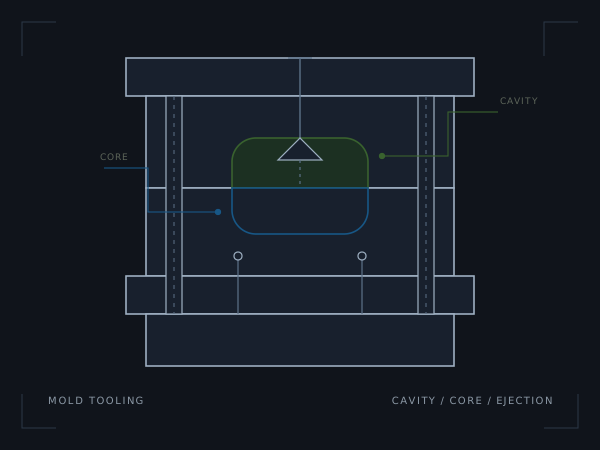
Mold cavity and core cross-section

Molds

Molds

Cavity and core work with design and build support for component production, including tool room machining and inspection.

Type
Cavity / core
Application
Plastic components
Support
Design + build
Request this tool

TAC PAL engineering

The part is the brief.

Tooling is one route. When the requirement starts earlier — a design, a sample, a machine decision or a batch of parts — these are the services that carry it.

01

Design & development support

We start with the function, then work back to geometry. Part design, tool design, feasibility checks and drawing support, with the manufacturing route considered from the first sketch.

  • Part design
  • Tool design
  • DFM review
  • Drawing support
02

Reverse engineering

A worn sample, an imported component or a part with no drawing. We measure, reconstruct and document the geometry, then establish what it will take to make it repeatably in India.

  • Sample measurement
  • CAD reconstruction
  • Localisation
  • Documentation
03

Machine consultation

Machine selection, tooling compatibility, process capability and cost reviews. We look at the whole route — machine, tool, material and maintenance — and leave a written action list rather than an opinion.

  • Machine selection
  • Process review
  • Tooling compatibility
  • Action plan
04

Prototyping & sample development

First-off samples and prototype parts before you commit to production tooling. Useful for fit checks, customer approval and proving a process before the capital is spent.

  • Prototypes
  • First-off samples
  • Fit checks
  • Pre-production
05

Precision manufacturing & job work

VMC machining, CNC turning, wire EDM, cylindrical and surface grinding, supported by precision inspection. Tool components, production parts and job work for manufacturers.

  • VMC
  • CNC turning
  • Wire EDM
  • Grinding
  • Inspection

How we work

Five steps. No surprises.

The sequence is deliberate. Most tooling failures are decided before the first cut — in an assumption that was never checked.

01

Understand

Drawing, sample, press, material and volume. We ask for what is missing.

02

Design

Tool concept, strip layout and feasibility. The manufacturing route is part of the design.

03

Build

Machining, assembly and inspection, with the tool room and metrology on the same site.

04

Trial

First-off part, load test where required, measurement and correction before release.

05

Support

Regrind, maintenance and the next change. The tool has a life after the handover.

Catalogues

Take the numbers with you.

Short PDFs covering the tooling families, press brake data and engineering services. For a drawing-specific proposal, send the part.

TOOL PAL tooling catalogue PDF · 2 pages · Tooling families
Download
Press brake tooling data PDF · 2 pages · 1000 kN/m · V12
Download
TAC PAL engineering services PDF · 2 pages · Services & process
Download

A drawing-specific answer

Send the part. We will specify the tool.

Press, material, thickness, feature and volume are enough for a first conversation. If you have the drawing, send that too.